Tag Archive for: Reliability
 Application Notes
Phonon Engineering and Advanced Thermal Management in Power Electronics
Phonon Engineering and Advanced Thermal Management in Power Electronics
From phonon-scattering physics to next-generation TIMs, substrate ceramics and active thermal control in SiC/GaN converters
Executive summary
Thermal management, together with reliability, is the factor that limits power density and useful life of power-electronics converters. The transition to wide-bandgap semiconductors (SiC and GaN) does not solve this problem — it shifts it: more efficient devices generate less heat, but over smaller die areas they produce more concentrated heat fluxes. The bottleneck, once again, is how to evacuate that heat without penalising reliability or introducing thermo-mechanical failure mechanisms.
Contemporary solid-state physics offers a set of conceptual tools — phonon-scattering engineering, Phonon-Glass Electron-Crystal (PGEC) materials, nanostructured superlattices — that have traditionally been developed to improve the thermoelectric figure of merit ZT. The underlying principles, however, are the same ones that govern the design of any advanced cooling system and any waste-heat recovery strategy. This article synthesises the academic state of the art and translates it into the decisions that a designer of industrial and railway inverters will be making in the coming years.
1. The thermal problem of power electronics
The junction temperature Tj of a power semiconductor simultaneously dominates electrical performance, useful life and reliability. The rule every power electronics engineer knows is brutal: for every 10 °C increase in Tj, the life of the power module drops to roughly half by the Arrhenius law; and for every 30 % increase in the thermal cycle amplitude ΔTj, the wire bonds of the module lose a factor of 3 to 5 in cycles to failure according to the Coffin-Manson model.
The most efficient reliability lever is not selecting better components, but reducing both Tj and ΔTj. And that reduction depends on the quality of the entire thermal chain — junction to case, case to heatsink, heatsink to ambient. Each of those links is a thermal resistance Rth in series, and improving it requires understanding what carries heat and what scatters it. Better cooling is not a fluid-mechanics problem solvable with bigger fans; it is, ultimately, a problem of how phonons propagate, scatter and dissipate.
2. Heat carriers — phonons and electrons
In any solid, heat is transported by two parallel mechanisms: the diffuse flow of free electrons (relevant in metals and degenerate semiconductors) and the propagation of crystal-lattice vibrations, quantised as phonons (dominant in insulators and non-degenerate semiconductors). Total thermal conductivity decomposes as κ = κe + κL.
2.1 The kinetic approximation and its limits
The classical phenomenological estimate is κ = (1/3)·C·v·l, where C is specific heat capacity, v the mean carrier velocity and l the mean free path between collisions. A rigorous analysis starts from the Boltzmann transport equation in the relaxation-time approximation. Electronic thermal conductivity is κe = (1/T)·[K₂ − K₁²/K₀], where the generalised transport integrals Kn capture the interplay between electrical conductivity σ, Seebeck coefficient α and κe. Thermoelectric design is, in essence, a vector optimisation problem.
2.2 Failure of the Wiedemann-Franz law
The Wiedemann-Franz law states κe/σT = L₀ = constant. It holds when electrons scatter through elastic (horizontal) processes. At intermediate temperatures, vertical inelastic processes appear: electrons relax through collisions with low-energy phonons that change carrier energy without significantly altering wave vector k. The net effect is that κe drops more aggressively than σ, and the actual Lorenz number falls below L₀.
For an inverter designer, this subtlety is tangible: simple kinetic thermal models overestimate the heat-transport capability of electrons at intermediate temperatures. In copper or aluminium DC bus bars operating in the 80–150 °C range typical of a railway inverter, vertical processes affect the real thermal balance — not an academic correction.
3. Lattice thermal conductivity and phonon scattering
In semiconductors and ceramics — the materials that make up the thermal path of a power module, from the SiC chip to the AlN substrate via the SAC305 solder — thermal conductivity is dominated by κL.
3.1 The Callaway model and Umklapp processes
The Callaway model integrates two types of phonon-phonon process. Normal (N) processes conserve crystal momentum and produce no direct thermal resistance; Umklapp (U) processes involve total momentum “wrapping around” outside the first Brillouin zone and are the primary source of intrinsic thermal resistance at temperatures comparable to or above θD.
Slack derived the U-process relaxation rate as τU⁻¹ ≈ (ℏγ²/Mv²θD)·ω²·T·exp(−θD/3T), where γ is the Grüneisen parameter — quantifying crystal anharmonicity — and M is the mean atomic mass. Design consequence: materials with high γ show high κL degradation with temperature; materials with high M scatter phonons at lower frequencies. This is why Bi₂Te₃ (high M) outperforms Si (high κ) as a thermoelectric despite similar crystal structures.
4. Phonon-Glass Electron-Crystal (PGEC) materials
The PGEC paradigm, formulated by G. A. Slack in the early 1990s, summarises the goal of modern thermoelectric engineering: an ideal material should transport electrons like a perfect crystal (high mobility, high σ) and transport heat like an amorphous glass (low κL). Forcing coexistence requires structures where unit-cell complexity acts as a selective phonon filter.
4.1 Skutterudites — the rattler mechanism
Skutterudites (general formula MX₃, M = Co, Rh, Ir; X = pnictogen) contain large icosahedral cages that host guest atoms. When a high-mass electropositive atom is introduced (lanthanides such as La, Ce, Yb; alkaline earths such as Ba), the guest is weakly bound and vibrates with anomalously large amplitude at a characteristic Einstein temperature θE — it literally rattles within the cage. This resonant scattering strongly suppresses phonons near the rattling frequency, reducing κL by up to an order of magnitude without proportionally affecting σ.
State of the art: double-filled skutterudites (Yb + Ba) have reached ZT > 1.5 at 800 K, compared with ZT ≈ 0.3 for the unfilled binary skutterudite — a 5× improvement obtained by engineering the same crystal with guest-atom insertion alone.
4.2 Clathrates
Clathrates (Types I, II, III, defined by cage geometry) operate under a similar principle with a more rigid and structurally complex host lattice. The reduction of κL is exacerbated by intrinsic guest disorder and the multiplicity of scattering centres in the unit cell — typically an order of magnitude lower κL than the host material without guests.
5. Nanostructuring and superlattices
The second great lever for reducing κL without destroying σ is nanostructuring. The fundamental idea is to introduce artificial boundaries at a scale that limits the phonon mean free path (λph typically 100–300 nm at room temperature) without significantly affecting that of electrons (λdB ~10 nm in degenerate semiconductors). The result is selective scattering: phonons blocked, electrons passing.
5.1 Kapitza resistance and coherent transport
At any interface between two materials with different vibrational properties — for example, Si/SiGe in a superlattice — phonons encounter thermal boundary resistance (Kapitza resistance, RB). The physical origin is the disparity between the dispersion relations ω(q) of the two materials. In superlattices with periods of a few nanometres, a qualitatively new phenomenon appears: the superlattice creates a new folded Brillouin zone with mini-gaps that block certain frequency ranges — a phononic crystal by analogy with photonic crystals.
5.2 Nanowires and low dimensionality
Reducing geometric dimensionality limits the phonon mean free path through surface scattering, especially when surfaces are rough. An emblematic case: graphite in 3D bulk form shows κ up to 2,000 W/m·K in the basal planes, but individual nanowires can show κ reduced by orders of magnitude through rough-surface scattering.
6. Practical implications for the inverter designer
The design-level view of the thermal chain (thermal budget, Foster/Cauer modelling, cooling hierarchy) is covered in our article Thermal Design in Power Electronics. Here we focus on what the physics of phonon transport adds to those decisions.
6.1 Thermoelectric recovery of waste heat
A 1 MW traction inverter at 95 % efficiency dissipates 50 kW of heat — comparable to an industrial electric heater. Advanced thermoelectric materials with ZT > 2 would open the possibility of recovering a non-negligible fraction as usable electricity, powering the converter’s own auxiliaries or returning it to the DC bus. On the 2028–2035 horizon, this represents a credible path to raising system efficiency above the 99 % plateau.
6.2 Advanced thermal interface materials (TIM)
The TIM layer between the power module and the heatsink is the most critical link in the thermal chain. Thermal conductivities by technology:
| TIM technology | κ (W/m·K) | Notes |
|---|---|---|
| Standard silicone grease | 1–3 | Outgassing risk in railway (optical, sensor environments) |
| Advanced ceramic pads | 6–10 | Current industrial standard |
| Phase-change metallised pads (PCM) | >12 | Premium PSU standard in railway programmes — no silicone migration |
| Dispersed graphene TIM | ~30 | Near-term commercial — qualification ongoing |
| Gallium-based liquid metals | 50–80 | Al compatibility challenges; high-power prototypes |
| Vertically aligned CNT | >100 | Research frontier — not yet at industrial maturity |
Premium PSU already standardises PCM pads in railway programmes where silicone is problematic (cabins with optical sensors, instrumentation equipment).
6.3 Substrate ceramics — the battle for high κ
The DBC (Direct Bonded Copper) substrate determines how much of the heat generated in the junction reaches the heatsink. Options ordered by increasing κ:
| Substrate | κ (W/m·K) | CTE (ppm/K) | Positioning |
|---|---|---|---|
| Al₂O₃ (alumina) | 24–26 | 7.0 | Cost-optimised industrial applications |
| Si₃N₄ (silicon nitride) | 70–90 | 3.2 | Gaining share — superior mechanical strength, severe thermal cycling |
| AlN (aluminium nitride) | 150–180 | 4.5 | Dominant in railway traction, industrial SiC |
| Diamond DBC | >1,000 | 1.5 | Research / aerospace — cost barrier for industrial use |
AlN is the dominant option in railway-traction modules and industrial SiC. Si₃N₄ is gaining share because it combines acceptable κ with superior mechanical strength — particularly important where DBC fatigue from thermal cycling is the dominant failure mechanism.
6.4 Active thermal management — the lever available today
While advanced materials mature, the lever with the best cost/benefit ratio available today is software-based active thermal management. Work by Andresen and Liserre (Microelectronics Reliability, 2014) demonstrates ΔTj amplitude reductions of 10–30 % through three control strategies:
Three control strategies for active thermal management
- Adaptive switching-frequency modulation — fsw is reduced under transient conditions to lower switching losses and relieve the most stressed module.
- Loss redistribution among parallel arms — the controller identifies the module with the highest Tj and shifts current towards less stressed ones.
- Real-time Tj estimation — from Vce_sat and current, with compensation by directly measured case temperature.
ΔTj-per-cycle reductions of 10–30 % translate, via Coffin-Manson, into 2–5× life-extension factors. This requires no novel materials and no manufacturing-process changes: it is implemented entirely in controller firmware. At Premium PSU we incorporate it progressively into higher-power platforms where the MTBF return justifies the additional control complexity.
7. Synthesis and outlook
Phonon-scattering engineering has proved to be the most effective route to overcome the limits of thermoelectric efficiency and, by extension, to rethink the foundations of thermal management in power electronics. Integrating the models of Klemens, Slack, Callaway and Pohl, the design of next-generation materials and architectures pivots on three pillars:
| Pillar | Mechanism | Horizon |
|---|---|---|
| Selective phonon scattering | Rattler atoms (skutterudites), cage disorder (clathrates), nanostructured interfaces | 2026–2030 — TIM and substrate integration |
| Phononic bandgap engineering | Superlattice folded Brillouin zones, coherent phonon blocking | 2030–2035 — module-level integration |
| Waste-heat recovery | Advanced ZT > 2 thermoelectrics, on-board TEG for auxiliaries | 2030–2035 — system level |
For the power electronics designer, the practical translation is clear: the physics developed to improve ZT in thermoelectrics is exactly the physics that governs next-generation TIMs, advanced substrates and active thermal management strategies. Understanding phonon transport is not an academic luxury — it is the foundation of the next decade of power-density and reliability improvements in power electronics.
About Premium PSU
Premium PSU (Premium SA) designs and manufactures custom power supplies and power converters in Barcelona, with over 40 years of experience in railway, energy, industrial, data centre and defence applications.
Talk to our engineering team
Discuss your power conversion requirements with Premium PSU.
 Application Notes
Advances in Power Electronics: Reliability and RAMS
Advances in Power Electronics: Reliability and RAMS
From the potentiometer to digital and laser trimming, from the electrolytic capacitor to software-based ripple control — a roadmap to 40-year reliability in critical infrastructure and railway
Executive Summary
Industrial and railway power electronics is going through a quiet but decisive transition: the replacement of electromechanical components and manual trimming techniques with solid-state architectures and deterministic calibration processes. Three levers drive this transition — the progressive elimination of the potentiometer, the reduction or elimination of the electrolytic capacitor, and the introduction of laser trimming on thick-film technology as the precision adjustment method in production. Each one targets a specific failure mechanism that historically limited converter service life; combined, they explain why a well-engineered unit today can be committed to an MTBF an order of magnitude higher than its fifteen-year-old predecessor at the same power rating.
This article walks through the three levers, ties them together with the Design for Reliability (DFR) methodology applied at Premium SA — mission profile, derating, FMEA, HALT/HASS, burn-in, FRACAS — and connects the result with the RAMS requirements of railway (EN 50126 / EN 50128 / EN 50129) and of critical grid infrastructure. The thesis is simple: 40-year reliability cannot be bought, it has to be designed; and the technological advances described here are the tools that make such a design viable.
1. The Paradigm Shift: From Reliability as Outcome to Reliability as Design Decision
For decades, the reliability of a power converter was measured after the fact. A unit was designed against a functional specification, manufactured, delivered, and the field failure rate was observed in service. If the number was unacceptable, the design was reworked. This “test-and-fix” approach has a well-known structural cost: correcting a reliability problem scales roughly 1× at schematic stage, 10× at layout, 100× at qualification testing, and grows by several additional orders of magnitude when the issue surfaces in a deployed fleet. The economics simply do not work in sectors with 30-year vehicle or substation lifecycles.
Design for Reliability (DFR), originated at the Center of Reliable Power Electronics (CORPE, Aalborg University) and adopted as the internal standard at Premium SA, inverts this order: reliability is set as a quantitative target at project kickoff — mission profile, target MTBF, service life, environmental conditions, thermal cycling — and the entire development process is structured to meet that number. The associated paradigm shift is the migration from handbook statistical models (MIL-HDBK-217F) toward a Physics-of-Failure (PoF) approach, grounded in the actual physical failure mechanisms: thermal fatigue of solder joints and wire bonds (Coffin-Manson), electrolyte evaporation under Arrhenius, electromigration, corrosion, mechanical fatigue of fasteners.
2. Goodbye to the Potentiometer: Digital Adjustment and Laser Trimming
2.1 The potentiometer as a concentrator of failure modes
The mechanical potentiometer has been the standard component for production calibration and field maintenance adjustments in power converters for half a century. Its appeal is obvious: it allows fine tuning of an analogue value (a voltage reference, a protection trip point, a gain) without changing components or reprogramming anything. But that very flexibility hides a concentration of failure mechanisms unmatched by any other passive component on the converter: mechanical wear of the resistive track; sensitivity to vibration (EN 61373 Cat. 1B); sensitivity to humidity and contamination; single point of intermittent failure via the wiper contact; and human risk in the adjustment — any manual field intervention is an opportunity to introduce an untraced calibration error.
The question is not whether a potentiometer will fail, but when. In a unit with a 30-year service life and a railway or substation mission profile, the answer is invariably “before the end”.
2.2 Replacement strategy 1 — digital potentiometer and parametric calibration
The first replacement strategy moves the adjustment to the digital domain. The analogue reference no longer comes from a trim resistor divider but is generated by software from a parameter stored in the microcontroller’s non-volatile memory or in an external EEPROM. Calibration is performed once in production, on a calibrated and traceable test bench, and is recorded against the unit’s serial number, operator, date and process signature.
| Characteristic | Mechanical potentiometer | Parametric digital calibration |
|---|---|---|
| Adjustment mechanism | Wiper sliding on resistive track | Read parameter from EEPROM/Flash |
| Temporal stability | Cumulative wear, vibration, humidity | Only DAC/MCU drift (ppm/°C) |
| Traceability | None beyond manual procedure | Digital log signed by serial number |
| Maintenance risk | Misalignment by human intervention | Protected calibration (digital signature) |
| Dominant failure mode | Intermittent wiper opening | MCU failure or EEPROM corruption |
| Typical function MTBF | < 50,000 h in harsh environments | > 500,000 h (silicon-limited) |
2.3 Replacement strategy 2 — laser trimming on thick film
Thick-film technology has matured to make laser trimming a standard industrial process. Modern resistive pastes (RuO₂ and advanced ceramic compounds) provide stable resistors up to 300 °C continuous operation, with temperature coefficients below ±25 ppm/°C in precision grades. Components produced this way are surge-resistant, mechanically robust and their value does not drift over time under normal operating conditions.
2.4 When to choose each strategy
| Function to be set | Preferred strategy | Reason |
|---|---|---|
| OVP/OCP/OTP trip points | Digital calibration | Mandatory traceability; RAMS audit |
| Control-loop gain | Deterministic design (no trim) | No post-design adjustment at all |
| Internal voltage reference | Laser-trimmed precision resistor network | Absolute stability without firmware involvement |
| Shunt current sensor | Laser-trimmed integrated resistor | 0.1 % tolerance with no temporal variation |
| Instrumentation amplifier gain | Laser-trimmed R2R network, IC-integrated | Current industry standard |
| Per-unit offset compensation | One-shot digital calibration in production | Covers natural silicon dispersion |
| Field-variable operating point | Signed digital parameter | Zero physical manual intervention |
The practical conclusion is that in a modern Premium SA control board there should be no physical potentiometer at all. Factory adjustments are laser or digital; field adjustments are digital-only, protected by signature; control loops are deterministic by design.
3. Reducing and Eliminating the Electrolytic Capacitor
3.1 The electrolytic as the Achilles heel of the DC bus
If the potentiometer is the Achilles heel of calibration, the aluminium electrolytic capacitor is the Achilles heel of the DC bus. It is typically the component that fixes the service-life ceiling of a power converter, because it combines five awkward properties: service life intrinsically limited by electrolyte evaporation (life ÷2 every +10 °C); ESR growing with ageing; capacitance decreasing to ~80 % at end-of-life; sensitivity to ripple current (Pdis = Iripple² × ESR → self-heating → accelerated ageing); and mechanical sensitivity requiring rigid restraint under EN 61373.
3.2 Premium SA strategy — long-life 105 °C capacitors
The first line of defence, when an electrolytic is unavoidable due to capacitance density, is aggressive part selection. Premium SA standardises on aluminium capacitors rated to 105 °C (some ranges to 125 °C in critical applications) with manufacturer-declared service life of 8,000 to 12,000 hours at maximum temperature — equivalent, by Arrhenius, to over 100,000 hours when operated at 50 °C. Combined with the Premium SA derating policy — Vop ≤ 80 % of Vrated, Iripple_real ≤ 80 % of Iripple_rated, Ta_cap < 85 °C in worst case — this pushes the ageing curve well below the product’s service-life horizon.
But “pushing” is not “eliminating”. As long as there is an electrolytic on the DC bus, there is a wear-out component that defines the slope of the bathtub curve at end of life.
3.3 Why digital ripple control changes the rules
| Aspect | DC bus with electrolytics | DC bus with film + digital control |
|---|---|---|
| Dominant component | Aluminium electrolytic 105 °C / 12,000 h | Polypropylene film, > 200,000 h |
| Dominant failure mechanism | Electrolyte evaporation (Arrhenius) | No significant wear-out mechanism |
| Thermal sensitivity | Life ÷2 every 10 °C | Minimal across operating range |
| Capacitance with ageing | Drops to 80 % at end of life | No significant drop |
| ESR evolution | Grows ×2 by end of life | Stable across full service life |
| DC-bus function MTBF | Limited by the electrolytic | Limited by semiconductors |
| TCO | Low BOM, high service cost | Higher BOM, lower service cost |
3.4 The measurable impact — MTBF, MTTR, reliability
Removing the electrolytic from the DC bus simultaneously moves all three metrics that matter in critical infrastructure. MTBF rises — we have observed typical 5× to 10× improvements in converters where the electrolytic was the limiting factor. MTTR drops because the LRU is replaced less frequently and the spare-parts catalogue is simplified. Reliability R(t) approaches 1 asymptotically over the full 30-year horizon, instead of degrading in the last 10 years due to electrolytic wear-out. These effects are particularly valuable where downtime carries contractual cost: an electrical substation where a fault triggers DSO penalties, or a rolling-stock fleet where a withdrawal from service breaks the operator’s timetable.
4. Design for Reliability — the Methodology that Ties the Advances Together
The two technological levers above are necessary but not sufficient conditions. 30-year reliability also requires a development process that integrates and verifies them. The Premium SA DFR methodology structures the design across four sequential gates — D2W (Design to Work), D2F (Design to Function), D4R (Design for Reliability) and D4Co (Design for Compliance) — each with quantitative exit criteria.
4.1 Mission profile and derating as non-negotiable input
The first artefact of any Premium SA project is the mission profile: maximum and minimum ambient temperature, daily thermal cycles, cyclic humidity, altitude, vibration, expected number of starts over the service life, frequency of S2 supply-interruption events. Without this input, no PoF calculation has any meaning. With it, derating decisions become quantitative.
| Component family | Premium SA derating rule | Physical justification |
|---|---|---|
| Power semiconductors | Tj ≤ 80 % of Tj_max (≤ 125 °C Si, ≤ 150 °C SiC) | Coffin-Manson on wire bonds: Nf falls as (ΔTj)^β |
| Aluminium electrolytics | Vop ≤ 80 % Vrated, Iripple ≤ 80 % rated | Arrhenius law on electrolyte evaporation |
| MLCC capacitors | Vop ≤ 50 % Vrated | Capacitance loss vs DC bias on X5R/X7R |
| Resistors | Pop ≤ 60 % Prated, Vop ≤ 80 % Vrated | Intra-component insulation |
| Connectors | I ≤ 70 % Irated per contact | Contact heating under fatigue |
| Insulation (creepage/clearance) | ≥ 1.5× minimum per EN 50124-1 | Margin against long-term contamination |
4.2 FMEA, FTA and the failure-mode hierarchy
Once derating is set, reliability engineering concentrates on identifying and mitigating the dominant failure modes through two complementary analyses. FMEA (Failure Mode and Effects Analysis) works bottom-up: for each component and each interface, possible failure modes, their causes and their effects are enumerated, with a Risk Priority Number assigned (RPN = Severity × Occurrence × Detection, 1–10 scale). At Premium SA, any RPN > 80 triggers a documented action plan, and RPN > 100 blocks the D4Co gate. FTA (Fault Tree Analysis) works top-down: it starts from the system failure and decomposes the Boolean combinations (AND/OR gates) that can cause it, allowing the impact of redundancies to be quantified and improvements to be prioritised by sensitivity factor.
4.3 The bathtub curve — each phase calls for a different technique
| Bathtub phase | Dominant cause | Control strategy |
|---|---|---|
| Infant mortality (0–500 h) | Latent manufacturing defects: cold solder, contamination, assembly errors | HALT in design + HASS/burn-in in production + 100 % AOI/ICT |
| Useful life (500–50,000 h) | Random events: overvoltage, ESD, mains transients | Protections (OVP/OCP/OTP), derating, preventive FMEA |
| Wear-out (> 50,000 h) | Accumulated damage: thermal fatigue, electrolyte degradation, corrosion | Low Tj_max, reduced ΔTj, eliminate electrolytics, condition monitoring |
4.4 HALT, HASS and burn-in — what each one does
These three techniques are often confused, and they tackle different problems at different moments. HALT (Highly Accelerated Life Testing) is a limit-exploration test in the design phase: combined stresses (temperature + vibration) are progressively applied beyond the specification, until the operational and destruct limits of the product are found. It is not a qualification test, it is a discovery test — the output is the knowledge of how much margin we hold. HASS (Highly Accelerated Stress Screening) is a production-phase variant, with stress levels chosen just below the operational limit, used to detect latent manufacturing defects without consuming the product’s service life. Burn-in operates the product under controlled temperature (typically +60 to +80 °C) and load for several hours to screen the infant-mortality phase. Premium SA standardises 4 h of burn-in per unit, extended to 8 h on programmes with long maintenance intervals.
The three are complementary: HALT explores; HASS screens in production; burn-in cuts the left tail of the bathtub curve. Applied together, the failure rate during the first year in service drops to a fraction of the value without these techniques.
5. The Other Component that Also Ages — the Software
Any modern converter with digital calibration, predictive ripple control, complex protections and communication with the network supervisor carries firmware of growing complexity. From the function-reliability standpoint, this firmware is just another component of the system — and like any other component, it can be the root cause of a failure that compromises availability. The difference is that software does not age physically, but confidence in it erodes if there is no disciplined verification and validation process.
5.1 V-Model and EN 50128 as the framework for railway firmware
The reference standard for railway-application software is EN 50128, part of the EN 5012x family (railway RAMS). Its central element is the V-Model: each level of specification (system requirements, software requirements, architectural design, module design, code) corresponds to a verification level (unit testing, integration testing, system testing, acceptance testing). Each SSIL (Software Safety Integrity Level, levels 1 to 4 plus Basic Integrity) imposes mandatory techniques: formal reviews, static analysis, specific coverage metrics.
| SSIL level | Typical converter application | Mandatory EN 50128 techniques |
|---|---|---|
| Basic Integrity | Functions unrelated to safety | Code review, functional testing |
| SSIL 1-2 | Cabin auxiliaries, monitoring | MISRA C static analysis, unit-test I/O coverage |
| SSIL 3 | Traction converters not brake-critical | MISRA + decision coverage + timing analysis |
| SSIL 4 | Active safety functions (e.g. brake inhibition) | MC/DC coverage, formal models, redundancy |
5.2 MISRA C, MC/DC and why they matter
MISRA C:2012 is the de facto standard for embedded firmware in C in critical systems. Its 143 rules (16 mandatory, 111 required, 16 advisory) cover language patterns that have historically been a source of defects: pointer aliasing, implicit conversions, undefined behaviour, dynamic memory management. Applying MISRA with static analysis (PC-lint, Coverity, Polyspace) removes a whole class of defects before execution. MC/DC (Modified Condition/Decision Coverage) is the most demanding coverage criterion routinely applied in certification: it requires that each individual condition within a Boolean decision independently affects the result of the decision. For a decision with n conditions, the minimum number of MC/DC tests is n+1, against the 2n required by combination coverage.
5.3 HIL and firmware verification on real hardware
The technique that closes the verification loop is HIL (Hardware-in-the-Loop). The firmware runs on the real microcontroller, but the input signals (voltage, current and temperature sensors) are synthesised by a real-time simulator that emulates the behaviour of the DC bus, the transformer, the motor or the load. This allows thousands of scenarios to be executed — including sensor failures, mains transients, short-circuits — with no physical risk to the equipment or to the test bench. A well-designed HIL programme catches hardware/software integration defects that no unit test could capture.
6. RAMS — the Metric that Ties Everything Together
RAMS stands for Reliability, Availability, Maintainability, Safety — the four metrics a railway operator or a grid DSO uses to judge the suitability of a unit across its service life. EN 50126 is the framework standard; EN 50128 and EN 50129 cover software and functional safety respectively.
6.1 The full R-A-M-S quadrant
| Metric | Operating definition | Dominant design lever |
|---|---|---|
| Reliability | Probability of fault-free operation across t | Component selection, derating, wear-out elimination |
| Availability | Fraction of time the system is operational | MTBF + MTTR; redundancy where applicable |
| Maintainability | Ease and speed of diagnosing and repairing | LRU design, telemetry, FRACAS, parts continuity |
| Safety | Absence of unacceptable risk | FTA, safe failure modes, software SSIL, redundancy of critical functions |
6.2 FRACAS — the continuous learning loop
FRACAS (Failure Reporting, Analysis and Corrective Action System) is the process by which every field return is analysed at the appropriate level — LRU, board, component — the root cause is identified, and the corrective action is propagated back to design and production. Premium SA runs FRACAS as a closed loop between Quality, Aftersales and R&D. The consequence is that the fleet population improves over time, rather than degrading: the issue detected in unit #150 is prevented in unit #151.
6.3 PHM and the move to predictive maintenance
The active technical frontier today is PHM (Prognostics and Health Management): the transition from fixed scheduled maintenance toward maintenance based on the actual condition of the equipment. In Premium SA converters we progressively implement: real-time Tj estimation of power semiconductors from Vce_sat and current; cumulative power-cycle counting with the associated ΔTj to predict RUL (Remaining Useful Life) via PoF models; capacitor ESR monitoring by ripple analysis; and periodic export of operational data to the operator’s supervisor over the communications bus. The result is that the operator no longer has to choose between excessive preventive maintenance and late corrective maintenance — the equipment reports how much life is left.
7. Synthesis: the Concrete Levers that Make 30-Year Reliability Viable
| Technological lever | Failure mode it removes | RAMS effect |
|---|---|---|
| Eliminating the potentiometer (digital + laser) | Wiper wear, vibration/humidity drift, human error in maintenance | Raises R, lowers MTTR |
| Reducing/eliminating the electrolytic (digital control + film) | Arrhenius wear-out of electrolyte | Raises MTBF 5–10×; flattens bathtub tail |
| Selection of 105–125 °C long-life electrolytics (where unavoidable) | Accelerated Arrhenius ageing of the limiting component | Pushes wear-out beyond the 30-year horizon |
| DFR + mission profile + derating | Random faults and overstress in the useful-life phase | Raises R in the central area of the curve |
| HALT in design + HASS/burn-in in production | Latent manufacturing defects (infant mortality) | Flattens the left tail of the bathtub curve |
| Software V&V (V-Model, MISRA, MC/DC, HIL) | Systematic firmware faults | The component that closes the case for a 30-year claim |
| LRU design + FRACAS + 30-year parts continuity | High MTTR and mid-life obsolescence | Raises A via the MTTR lever; protects the full lifecycle |
| PHM + condition monitoring | Inefficient maintenance (excessive preventive or late corrective) | Optimises total cost of ownership |
About Premium PSU — With over 40 years of experience, Premium SA designs and manufactures custom power converters in Barcelona for railway, energy, industrial, data center and defence applications.
 Application Notes
The First Prototype Admits No Second Chance
The First Prototype Admits No Second Chance
Why we simulate before soldering: the integrated simulation, quantitative reliability and accelerated test chain behind custom power electronics delivered on time.
Born in Barcelona, Powering the World
In power electronics for critical sectors — railway, defence, energy, digital infrastructure — the custom project does not allow the iterative cycle of the catalogue product. Production runs are short. Deadlines are contractually binding. The first prototype delivered to the customer is validated against the entire contract, not against a simplified preliminary version.
The consequence is structural: success at the first prototype is not a desirable goal, it is the condition that makes the business model work. When a railway customer needs a converter operating at −40 °C, or an AI application requires dissipating more than 700 W/cm² locally, the design cannot be closed “by eye”. Whether a project delivers at the first prototype or iterates three times is decided before the first PCB is manufactured.
The constraint that defines the sector
Typical production runs in custom railway or defence projects sit between 50 and 500 units. The product learning curve runs out before the cost of a partial redesign is covered, so the catalogue business model — amortising iteration over thousands of subsequent units — does not apply. Every deviation detected when validating the first prototype has three possible outcomes, all costly: redesign with replanning, acceptance of contractual penalties, or batch rejection with replacement.
The metric Premium SA uses internally to evaluate design-flow maturity is the first-pass approval rate of DVT (Design Verification Testing). When stages are shortened due to schedule pressure, the indicator drops rapidly and drags timelines and margins with it.
Four fault vectors, four models
Pre-hardware verification is structured in four layers covering the dominant fault vectors in power electronics.
Electrical modelling: SPICE, PLECS and Simulink
SPICE for detailed switching analysis, and PLECS or Simulink for full-system simulation, allow verification — before manufacturing the first PCB — that the closed loop is stable, that waveforms do not exceed semiconductor margins, and that losses are consistent with the available dissipation. For SiC or GaN topologies, accurately capturing packaging parasitic inductance is decisive: a use case of the European ALL2GaN research project has documented how TOLL versus PG-DSO-20 packaging conditions snubber sizing in 3 kW/48 V totem-pole rectifiers achieving 97.5% efficiency and 40 W/in³ density.
Thermal CFD simulation
From chip to system. Real density does not come from table coefficients. For local heat fluxes above 700 W/cm² in AI applications and current-generation OCP servers, integrated liquid microchannels with dielectric coolant, in fraction-of-a-millimetre channel geometries, are already production-ready technology.
EMC pre-compliance simulation
The chamber costs thousands of euros and calendar days; discovering a radiated-emissions failure with the product already wired is one of the most damaging scenarios in a custom project. Modern solvers allow prediction of compliance with CISPR 32, EN 50121-3-2 (railway) or MIL-STD-461 (defence) before manufacturing. The Premium SA criterion: a design margin of at least 6 dB with respect to the applicable limits.
MATLAB / Simulink for digital control
Verification of control-loop stability and automatic C code generation. For SIL2/SIL3 under EN 50128 or ASIL-B/C under ISO 26262, traceability between safety requirement, model and generated code is a normative requirement.
Beyond simulation: reliability by design and physical testing
Reliability is not only verified on the bench; it is designed. Quantitative reliability analysis — the D4R block in Premium SA’s D2x methodology — makes it possible to commit to contractual MTBF figures backed by model and evidence. Tools: Telcordia SR-332, MIL-HDBK-217F, Siemens SN29500 and FIDES, depending on the customer and sector; FMEA with quantitative RPN thresholds; FTA with PFH calculation for SIL3. We explain this approach in more depth in our white paper on reliability in critical power electronics.
Physical testing closes the loop: DVT on three units (all must pass without rework), HALT to identify operational and destructive margins, and HASS as a production filter for each manufactured unit. The HALT+HASS combination does not replace DVT; it complements it — DVT verifies the design, HALT identifies the margins and HASS ensures that each unit stays within them.
The first prototype as the threshold of the business model
The chain described — four layers of simulation, three quantitative reliability tools, two levels of accelerated testing, all structured by the D2x methodology with V-Model and quantitative stage-gates (D2W, D2F, D2C, D4R, D4Co) — is Premium SA’s operational answer to a structural constraint: the first prototype must work. The investment has a measurable return: every hour of correct modelling is an hour not spent — multiplied — on physical bring-up, production redesign or warranty.
For the customer engineer evaluating suppliers, the relevant question is not whether the supplier knows how to design; it is whether the supplier knows how to verify. In custom power electronics for critical sectors, this is not an efficiency improvement: it is the condition that sustains the project.
Normative references
| Standard | Scope |
|---|---|
| Telcordia SR-332 · MIL-HDBK-217F · SN29500 · FIDES 2022 | MTBF / reliability prediction methods |
| IEC 61508 · EN 50128 | Functional safety; PFH <10⁻⁷/h for SIL3 |
| ISO 26262 | Automotive functional safety (ASIL) |
| CISPR 32 · EN 50121-3-2 · MIL-STD-461 | EMC: multimedia equipment, railway rolling stock, defence |
Talk to our engineering team
Planning a custom converter for railway, defence, energy or digital infrastructure? Talk to our engineers about how the simulation and test chain is applied to your project from the first design gate.
About Premium SA
Premium SA (Premium PSU) is a Barcelona-based designer and manufacturer of custom power supplies and power converters for railway, energy, industrial, data centre and defence applications, with over 40 years of experience since its foundation in 1981. Born in Barcelona, Powering the World.
 Application Notes
Total Cost of Ownership (TCO) in Power Electronics: Why the Lowest Price Is Rarely the Best Decision
Total Cost of Ownership (TCO) in Power Electronics: Why the Lowest Price Is Rarely the Best Decision
The hidden costs that never appear on the quotation, a practical framework for calculating TCO and five questions for your next procurement process.
In many competitive evaluations of power converters, unit price is the number-one decision factor, while TCO (Total Cost of Ownership) analysis is applied in only a minority of cases. This means that most purchasing decisions are made without considering the costs that actually determine the long-term economic impact.
This article explains why unit price is a misleading indicator, which hidden costs are usually ignored, and how to apply a practical TCO analysis to your next supplier evaluation.
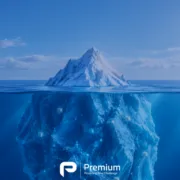
The iceberg model: what you don’t see is what costs most
The unit price of the converter is the tip of the iceberg: visible, easy to compare and apparently decisive. Beneath the surface, however, there are seven cost categories that in many cases exceed the purchase price by a factor of 3 to 10:
- Cost of field failure. A converter failure on a train does not cost EUR 1,000 for the replacement unit. It costs between EUR 10,000 and 55,000 once you add vehicle downtime (EUR 1,500–5,000/day), technician call-out (EUR 2,000–8,000), urgent shipping of the spare (EUR 500–3,000), root-cause investigation (EUR 5,000–15,000) and contractual service penalties.
- Integration engineering. Changing supplier is not simply swapping one unit for another. It involves requalification, EMC testing, mechanical integration and documentation updates. Typical cost: EUR 30,000–75,000 per model.
- Life-cycle support. A supplier offering 5 years of product availability for a vehicle with a 30-year service life is not saving you money: it is creating an obsolescence problem that will cost more than EUR 50,000 per model when the product is discontinued.
- Warranty and after-sales costs. More restrictive warranty terms (1 year versus 5 years) and longer response times translate into higher operating costs.
- Logistics costs. Lead times of 16 weeks from Asia versus 4 weeks from Europe. Higher safety-stock costs. Risk of delays from sea freight, customs and supply-chain disruption.
- Training and documentation costs. A supplier providing documentation in English, Spanish and German reduces training costs for maintenance staff.
- Supply risk. The 2021–2023 supply-chain crisis showed that dependence on distant suppliers can stall projects for 6–12 months.
How to calculate TCO: a practical framework
Calculating TCO does not have to be complex. For a practical evaluation, use this simplified formula:
TCO = unit price + (NRE / project units) + (failure rate × cost per failure × years of service) + (obsolescence cost / affected units) + logistics delta
Where:
- NRE is the non-recurring engineering cost (integration, qualification, documentation).
- The failure rate is derived from the equipment MTBF.
- The cost per failure includes all direct and indirect costs.
- The obsolescence cost is the redesign required when the product is discontinued.
- The logistics delta is the difference in inventory and transport costs between suppliers.
Example: when the cheapest converter costs twice as much
Consider two quotations for a railway DC/DC converter in a 200-unit project with a 25-year service life:
| Item | Supplier A | Supplier B |
|---|---|---|
| Unit price | EUR 800 | EUR 550 |
| Declared MTBF | 100,000 h (MIL-HDBK-217F, 40 °C) | 60,000 h (Telcordia, 25 °C) |
| Warranty | 5 years | 2 years |
| Product availability | 20+ years | 7 years |
| Lead time | 4 weeks (Europe) | 16 weeks (Asia) |
Supplier B looks 31% cheaper. But when TCO is calculated, Supplier B’s real MTBF (adjusted to MIL-HDBK-217F at 40 °C) is approximately 25,000 hours, which means 4 times more field failures. The total cost of failures over 25 years is 3–5 times the unit-price saving. In addition, Supplier B will require at least 3 obsolescence redesigns over 25 years (cost: EUR 90,000+).
Result: Supplier B’s TCO is 40–60% higher than Supplier A’s.
Five questions for your next procurement process
Build these questions into every power-electronics supplier evaluation:
- Give me the MTBF according to MIL-HDBK-217F at 40 °C ambient. If the supplier cannot or will not, ask yourself why.
- What is your written commitment on spare-part and product availability? Accept only contractual commitments, not verbal ones.
- What is your obsolescence management plan? When a key component reaches end of life, what is the process and who bears the cost of the redesign?
- What is your real lead time and where do you manufacture? If the project cannot absorb a 4-week transport delay, you need European manufacturing.
- Give me a TCO breakdown, not just the unit price. The suppliers who can do this, and are willing to, are the ones worth having as partners.
These five questions will steer your supplier list towards companies that deliver long-term value, not just short-term savings. To go deeper into how reliability is designed in to reduce TCO, see our white paper on reliability in critical power electronics.
Want to apply a TCO analysis to your next supplier evaluation? Our technical team can help you quantify the hidden costs.
About Premium PSU
Premium PSU (Premium SA) designs and manufactures custom power supplies and power converters in Barcelona, with over 40 years of experience in railway, energy, industrial, data centre and defence applications.
Talk to our engineering team
Discuss your power conversion requirements with Premium PSU.